
Brass CNC Machining Factory: How the Floor Proves Alloy, Conductivity, and Compliance on One Order
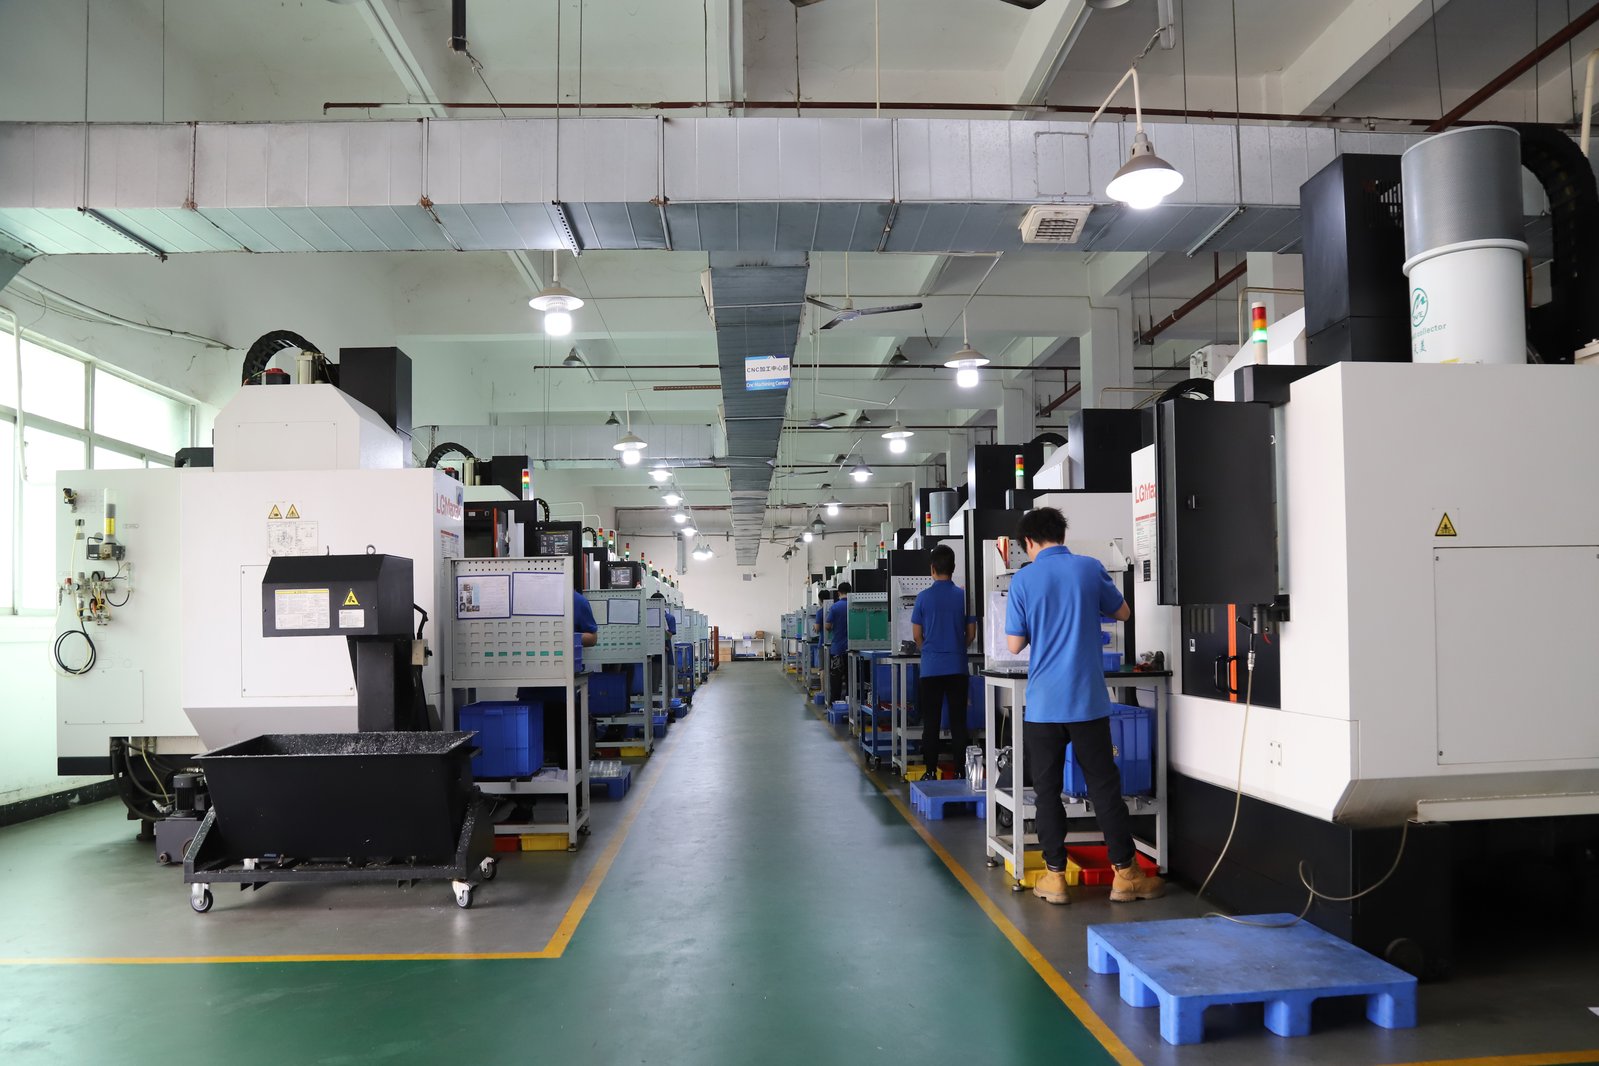
Brass parts get ordered for reasons a standard machining quote does not address: electrical conductivity, corrosion resistance, non-sparking behavior in hazardous areas, and a machinability that other metals envy. Those properties are only as real as the factory's control over them. A brass CNC machining factory earns its name by proving three things on every order, that the incoming stock is the grade on the certificate, that machining and finishing preserve the property your part exists for, and that the batch record ties the two together. This guide is the buyer's version of that audit: which grades to name on the drawing, what to verify when the stock lands, what changes on the factory floor when the material is brass, and what the shipped file must contain before you release repeat volume.
The short answer: audit the factory on brass-specific lines before you send a drawing. Confirm it XRF-verifies incoming copper-alloy stock against the certificate, that it machines brass with the chip control and tooling the metal actually needs, that it knows which finishes destroy conductivity and which preserve it, and that the batch record carries the material evidence through to the dimensional report. On each line, ask for the record, not the reassurance.
Why does a brass part change which factory you should audit?
Most machining audits ask the same questions regardless of material: what machines, what tolerances, what certificates. Brass rewards a narrower audit, because the metal's value sits in properties that a dimensional report cannot see. A connector body can measure perfectly and still be the wrong alloy, carrying the wrong lead content, or plated in a way that turns a conductor into an insulator. The claims that matter on brass — composition, compliance, and conductivity — are verified through material records and process choices, not through a CMM.
The factory question is therefore not "can you cut brass?" — every shop with a spindle can. It is whether the floor controls the three things a brass part depends on: the grade that entered the building, the finishing step that followed the cut, and the documentation that ties the two to your lot number. That is the difference between a brass CNC machining factory and a shop that happens to run brass between steel jobs.
Which brass grade should your drawing name, and what does each demand?
Brass is a copper-zinc family with a wide performance spread, and the grade on the drawing decides both the part's function and the factory's job. The floor behind this site lists brass and copper among its regular materials — C360, H62, and C110 appear in the materials table on the services page, which is the level of specificity a buyer should expect before sending a drawing that says only "brass."
- C360 — the free-cutting standard. The classic leaded free-machining brass, carrying roughly 3 percent lead by weight. It is the default for high-volume turned and milled parts because it cuts fast, holds fine threads, and produces clean surfaces. Its lead content is exactly what triggers compliance questions in electronics and potable-water applications.
- H62 — the Chinese-designated copper-zinc grade. Named for its roughly 62 percent copper content, it is widely specified on drawings that follow Chinese material practice, and it is what many Dongguan shops keep in routine stock. When your drawing follows GB/T practice, H62 is the designation a local factory reads without translation.
- C110 — high-conductivity copper. Not technically a brass but the same copper-alloy family, used where conductivity matters more than strength — bus bars, terminals, and current-carrying parts. C110 demands care in machining because pure copper is gummy; it does not break chips the way leaded brass does.
The buyer's rule is the same one that applies to every metal: name the grade on the drawing, and confirm the factory actually runs it. "Brass" on a print invites whatever bar is cheapest on the day; "C360" or "H62" fixes the composition, the machinability, and the compliance conversation in one line.
How does a factory verify the brass lot is what the certificate says?
Brass arrives with a mill certificate that names the alloy and its copper, zinc, and lead content. The certificate is a claim; the verification is a measurement on the actual stock. On copper alloys, X-ray fluorescence reads the elemental mix — copper, zinc, lead, and the trace elements that distinguish one grade from another — so an XRF check at intake catches the two failure modes a certificate alone cannot: a substituted grade and a mixed lot.
This is the material-control step documented on the quality system page for the floor behind this site, and it is the first thing to ask about on a brass order. The incoming lot is read against its certificate before the metal reaches a machine, and the check is recorded as part of the lot record — dated, tied to the certificate, and retrievable. On lead-restricted grades, the same check matters doubly, because the lead content is the property that makes the part legal or not in its destination market. A buyer should be able to ask "what was the verified composition of the lot my parts came from" and get a number, not a sentence.
One boundary is worth knowing before you rely on the check: XRF identifies the elements present, and it separates C360 from C110 cleanly because the copper-zinc-lead mix differs sharply. It is less useful as a substitute for the certificate on trace elements that sit below a fraction of a percent, and it will not tell you about mechanical condition such as temper or hardness. The certificate and the XRF read are complements, not alternatives — the certificate states what the mill produced and tested, and the XRF read confirms the bar on your floor matches it. Ask for both, tied to the same lot, and the material gate on a brass order is closed.
What changes on the factory floor when the material is brass?
Brass machines beautifully, that is its reputation and its trap. Because it cuts easily, a factory can run it fast and still hold good geometry, which is why leaded brass is the reference standard for machinability. The floor-level disciplines that separate a real brass operation are the ones that protect the part and the process rather than the spindle speed:
- Chip control. Long, stringy chips wrap around tools and workpieces, scoring finished surfaces and stopping automated cycles. A brass shop controls chip formation with the right insert geometry and coolant delivery, and it manages the swarf — on copper alloys the chips carry real scrap value, so they are segregated and collected rather than swept into the general bin.
- Tooling that matches the grade. Leaded C360 cuts with almost no resistance, which lets a factory hold fine finishes and tight tolerances at high feed. Pure copper and low-lead alloys behave differently — they are softer, gummier, and more prone to built-up edge — so the tooling and speeds that work for C360 do not transfer automatically.
- Burr and edge control. Brass's softness means the exit edge of a cut is where burrs form, and on electrical parts a burr can bridge two contacts that must stay isolated. Deburring and edge breaking on brass are functional operations, not cosmetic ones.
When you evaluate a factory for brass, ask how it runs the specific grade on your drawing. A floor that has machined C360 terminals by the thousand will answer with feeds, tooling, and cycle times; one that treats brass as "like aluminum, but heavier" has not thought about the metal at all.
Which finishing steps preserve a brass part's conductivity, and which destroy it?
The property most brass parts are ordered for is electrical conductivity, and the finishing decision is where that property is won or lost. The rule that surprises most buyers: anodizing, the default finish on aluminum, does not exist for brass, and the finishes that substitute for it are not all conductive.
A conductive brass part should stay bare, or receive a thin conversion or plating that does not insulate the contact surfaces. Chromate conversion and bright dips preserve conductivity while protecting against tarnish; plating with tin, nickel, or gold is specified where the application demands solderability, wear, or corrosion resistance, and where a plated layer is a deliberate part of the electrical design rather than an afterthought. What the factory must not do is apply a thick organic coating to a part that must carry current, or plate over surfaces that must make electrical contact, without the drawing saying so.
The drawing should therefore state which surfaces are functional contacts and which are cosmetic, and the factory should plan masking accordingly. On a brass order, the finishing spec is not a surface detail — it is a functional requirement, and it belongs in the record the same way a dimension does.
What tolerance and inspection evidence should a brass order carry?
Brass will hold whatever tolerance the process is set up and verified for; the discipline is the same as on any precision metal. The floor behind this site holds ±0.003 mm on CNC milling and turning and ±0.002 mm on precision grinding, verified on in-house Hexagon CMMs, with key characteristics charted to Ppk ≥ 1.67 initial. The evidence a brass buyer should demand is the evidence any precision buyer should demand, with one material note added:
- A dimensional report with measured values against the drawing — "OK" is an opinion, "10.0013 mm" is a measurement.
- SPC where characteristics are critical, showing the process held the tolerance across the batch rather than on the first article.
- The material record alongside the dimensional one — on brass, the certificate and the XRF verification belong in the same file as the CMM report, because a part that measures right and is the wrong alloy has failed in a way no caliper can see.
Temperature matters on brass as it does on every metal: measurement at a controlled reference temperature is what makes a reported dimension mean something on your assembly line. Ask how the factory measures, not just what it claims to hold.
What should the lot file contain when brass parts ship?
The shipment file is where the brass order proves itself, and it should tie four things to one lot number:
- The mill certificate for the actual heat — alloy, composition, and the standard it was produced to.
- The XRF verification record — the incoming check that matched the stock to the certificate, with a date.
- The inspection evidence — CMM reports with measured values against the drawing, and SPC where key characteristics are charted.
- Compliance documentation where the destination requires it — composition evidence for lead-restricted grades destined for electronics or potable-water markets, named as a deliverable rather than assumed.
All four should reference the same lot number and drawing revision, so the file describes your order rather than the factory's general capability. A documentation package that cannot be matched to a lot is a brochure; one that matches is the difference between a supplier you can audit and one you have to trust.
Which questions should you put to a brass machining factory before the PO?
The questions that screen a serious brass CNC machining factory are the ones that test the material record and the process discipline, not the sales page:
- Which brass grades do you run, and is mine among them? The answer should name C360, H62, or your grade's equivalent, not "we do brass."
- What happens to the copper-alloy stock when it arrives? An XRF check against the certificate, recorded per lot — the same material-control step the quality page documents.
- How do you machine the grade on my drawing? The answer should mention chip control and tooling for that specific alloy, because C360 and pure copper demand different setups.
- Which surfaces are conductive on my part, and how do you protect them through finishing? A shop that understands brass will ask you to define the contact surfaces before it quotes a finish.
- What tolerance evidence ships with the parts? Measured values on a CMM report, tied to the drawing, at a stated reference temperature.
- What compliance documents accompany the material? On lead-restricted grades, the composition evidence should be a named deliverable, not a favor.
Send these by email before you send the drawing. A factory that answers with instruments, records, and process detail is running the system your brass part depends on; one that answers with assurances is asking you to be its quality department.
Frequently Asked Questions
Which brass alloys do you machine?
We machine C360 free-cutting brass, H62 copper-zinc, and C110 high-conductivity copper as part of a regular copper-alloy program, alongside the stainless, alloy steel, aluminum, and engineering plastics we run. Every incoming copper-alloy lot is XRF-verified against its mill certificate before it reaches a machine.
What is the minimum order quantity for brass CNC machined parts?
One piece. A single-part brass order is the cheapest way to test the three things that matter — the material record, the finishing decision, and the dimensional evidence — before you commit a production batch to the same process.
Does anodizing work on brass parts?
No — anodizing is an aluminum process and does not apply to brass. Conductive brass parts are finished with thin conversion treatments (such as chromate) or plated where the application demands solderability or corrosion resistance, and functional contact surfaces should be defined on the drawing so the factory can mask and protect them.
What tolerances can brass CNC machining hold?
We hold ±0.003 mm on CNC milling and turning and ±0.002 mm on precision grinding, verified on Hexagon CMMs, with key characteristics charted to Ppk ≥ 1.67 initial. Inspection runs at a controlled reference temperature so the numbers mean something in your assembly.
How do I verify the brass in the parts I receive is the grade I ordered?
By the lot record: the mill certificate names the alloy and its composition, an XRF check at intake verifies the actual stock against the certificate, and the batch identity ties the finished parts back to that lot. Dimensional inspection cannot see chemistry, so the material record is the only proof.
Does lead content affect where I can sell brass parts?
Yes. Free-cutting brass such as C360 carries roughly 3 percent lead, and lead is restricted in the markets where brass parts are most used — electronics under RoHS-type rules and potable-water fittings under strict lead limits. The destination market's requirement should drive the grade choice and the compliance evidence, and the drawing should state it.
Which certifications does the factory hold?
Dongguan Zhuohang Ltd holds ISO 9001:2015 (No. 116024/A/0001/UK/En), IATF 16949:2016 (product design excluded) (No. 131941/A/0001/SM/En), and ISO 14001:2015 (No. 116024/B/0001/UK/En). The IATF scope is build-to-print, and the certificates are verifiable by number with the registrar rather than by logo.
Putting a brass drawing out to a factory and want the material record to prove it?
Send the drawing with the grade, the compliance requirement, and the conductive surfaces marked, and we will return a quote with the process, the finishing scope, and the documentation package spelled out. Email [email protected] or call +86 13126536955.